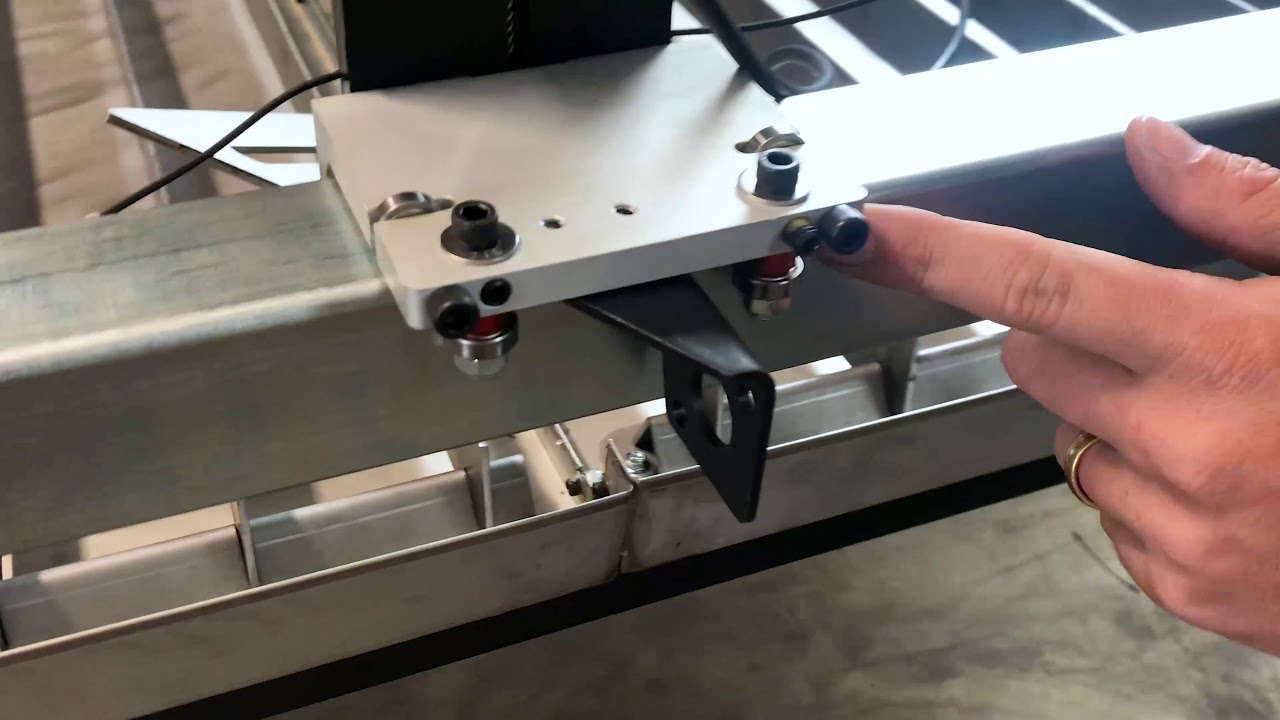
First cut of the day sank into the water table with one end up just right for the torch assembly to catch and actually push the bottom V-rollers right off of the gantry. The top V-rollers seem to be right where they should be indicated by them still on the worn path but the bottoms are pushed out far enough that the nuts on the backside are where the rollers should be.
This part was pre-assembled in the box from what I remember, pretty sure I only had to slide it onto the gantry when I put the table together. What steps should I take to get this back into position?
There are set screws you go back and forth with as you add/remove preload for those bearings to get your Z-axis assembly perpendicular to your cutting surface.
I would simply remove the assembly and clean it all up before reinstalling it and tramming.
As others have already stated back out the grub screws to roller adjustment, but also them roller bolts are lose snug up bolt and nut but don’t over tighten bolt and nut. Because when you set bearing preloads by tightening the grub screw it pushes against bolt so bolt has to move, want some tension on bolt.
Go to assembly video shows how to tram those bearings.
Thanks for all the replies fellas, lots of good info here. I thought that this was going to be much more of a headache but loosening those set screws gave me the tolerance to simply set the assembly back into place. Gave everything a good cleaning and relubricating before aligning and tightening it all back up. My x-z assembly is trammed and now moving along both axes smoother than ever before.
Just in case anyone else has this issue: I had some extra wiggle in the torch head that was driving me nuts until I realized that one (and only one) specific screw holding the torch head V-block to the z-axis slide has an area flattened to dial in how tight the torch is held. I tightened it too much at first and the torch wouldn’t go low enough to penetrate cuts but after backing off a little it’s doing fantastic.
Now if I could only work out why the THC sends the torch head to the moon once in awhile. Seems mostly random but almost always after the torch is making a corner around a long cut. Most of the time I can run new code from the last LINE and it will cut fine but not always. I suspect that maybe it’s something going on in the THC torch cutoff setting or maybe just a g-code flaw? Has anyone had that issue and been able to solve it?
If your torch jogs upward, pay attention to Firecontrol and see if IHS initiates at all.
If IHS is triggered, whether it’s a sticky Z-axis assembly, dirty contacts, or something else, it will initiate the probing sequence in that it zeroes out your position and jogs upward for your programmed cut height. Triggering several times is what causes it to jog up.
I’ve also heard of EMI causing this but that’s a bit more difficult to tackle in some situations.
IHS can trigger while the torch is moving? I didn’t know that, I’ll have to keep an eye out for when the torch starts jogging up so far that it loses the arc. My table is plugged into the same double gang as the desktop pc that I’m running FC on and the cable connecting the two has always had those snap on chokes with the isolator dongle. Would separating either the table or desktop to another outlet eliminate chances of EMI?