Plasma cutting .25" aluminum

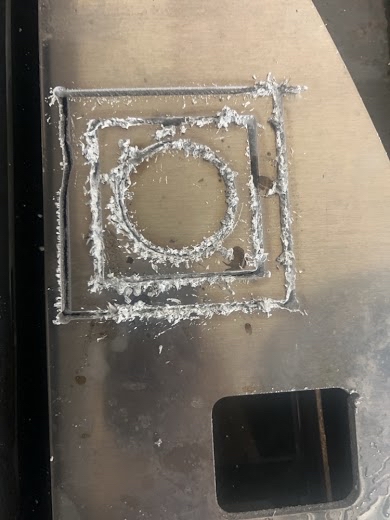
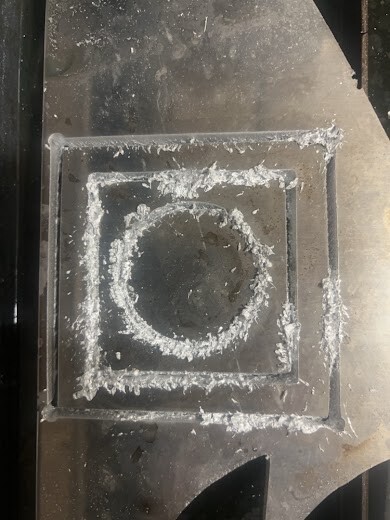
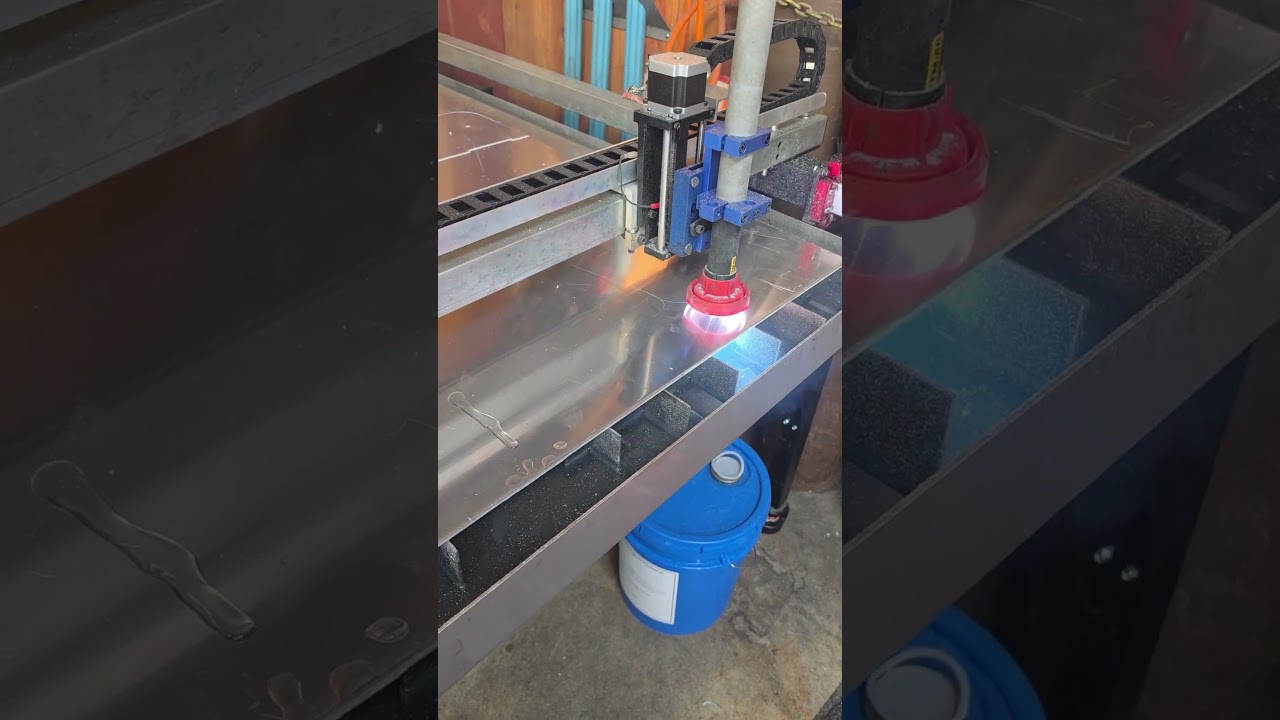
So, our school has a Langmuir Crossfire XR and a Hypermax 45. We are trying to cut .25" aluminum and are having a lot of issues with cutting.

Current (Amps) 45 A
Shielded Consumables Standard 45A Shielded
Cut Speed 40ipm
Cut Height 0.060"
Pierce Height 0.150"
Pierce Delay 1.3s
Kerf Width 0.065"

Please Help us if you can

It looks like the work clamp isn’t connected. Check the consumables. Send me pictures of the ends. Sometimes aluminum globs get stuck to the torch tip. This messes with the cut height. Your settings are pretty close.

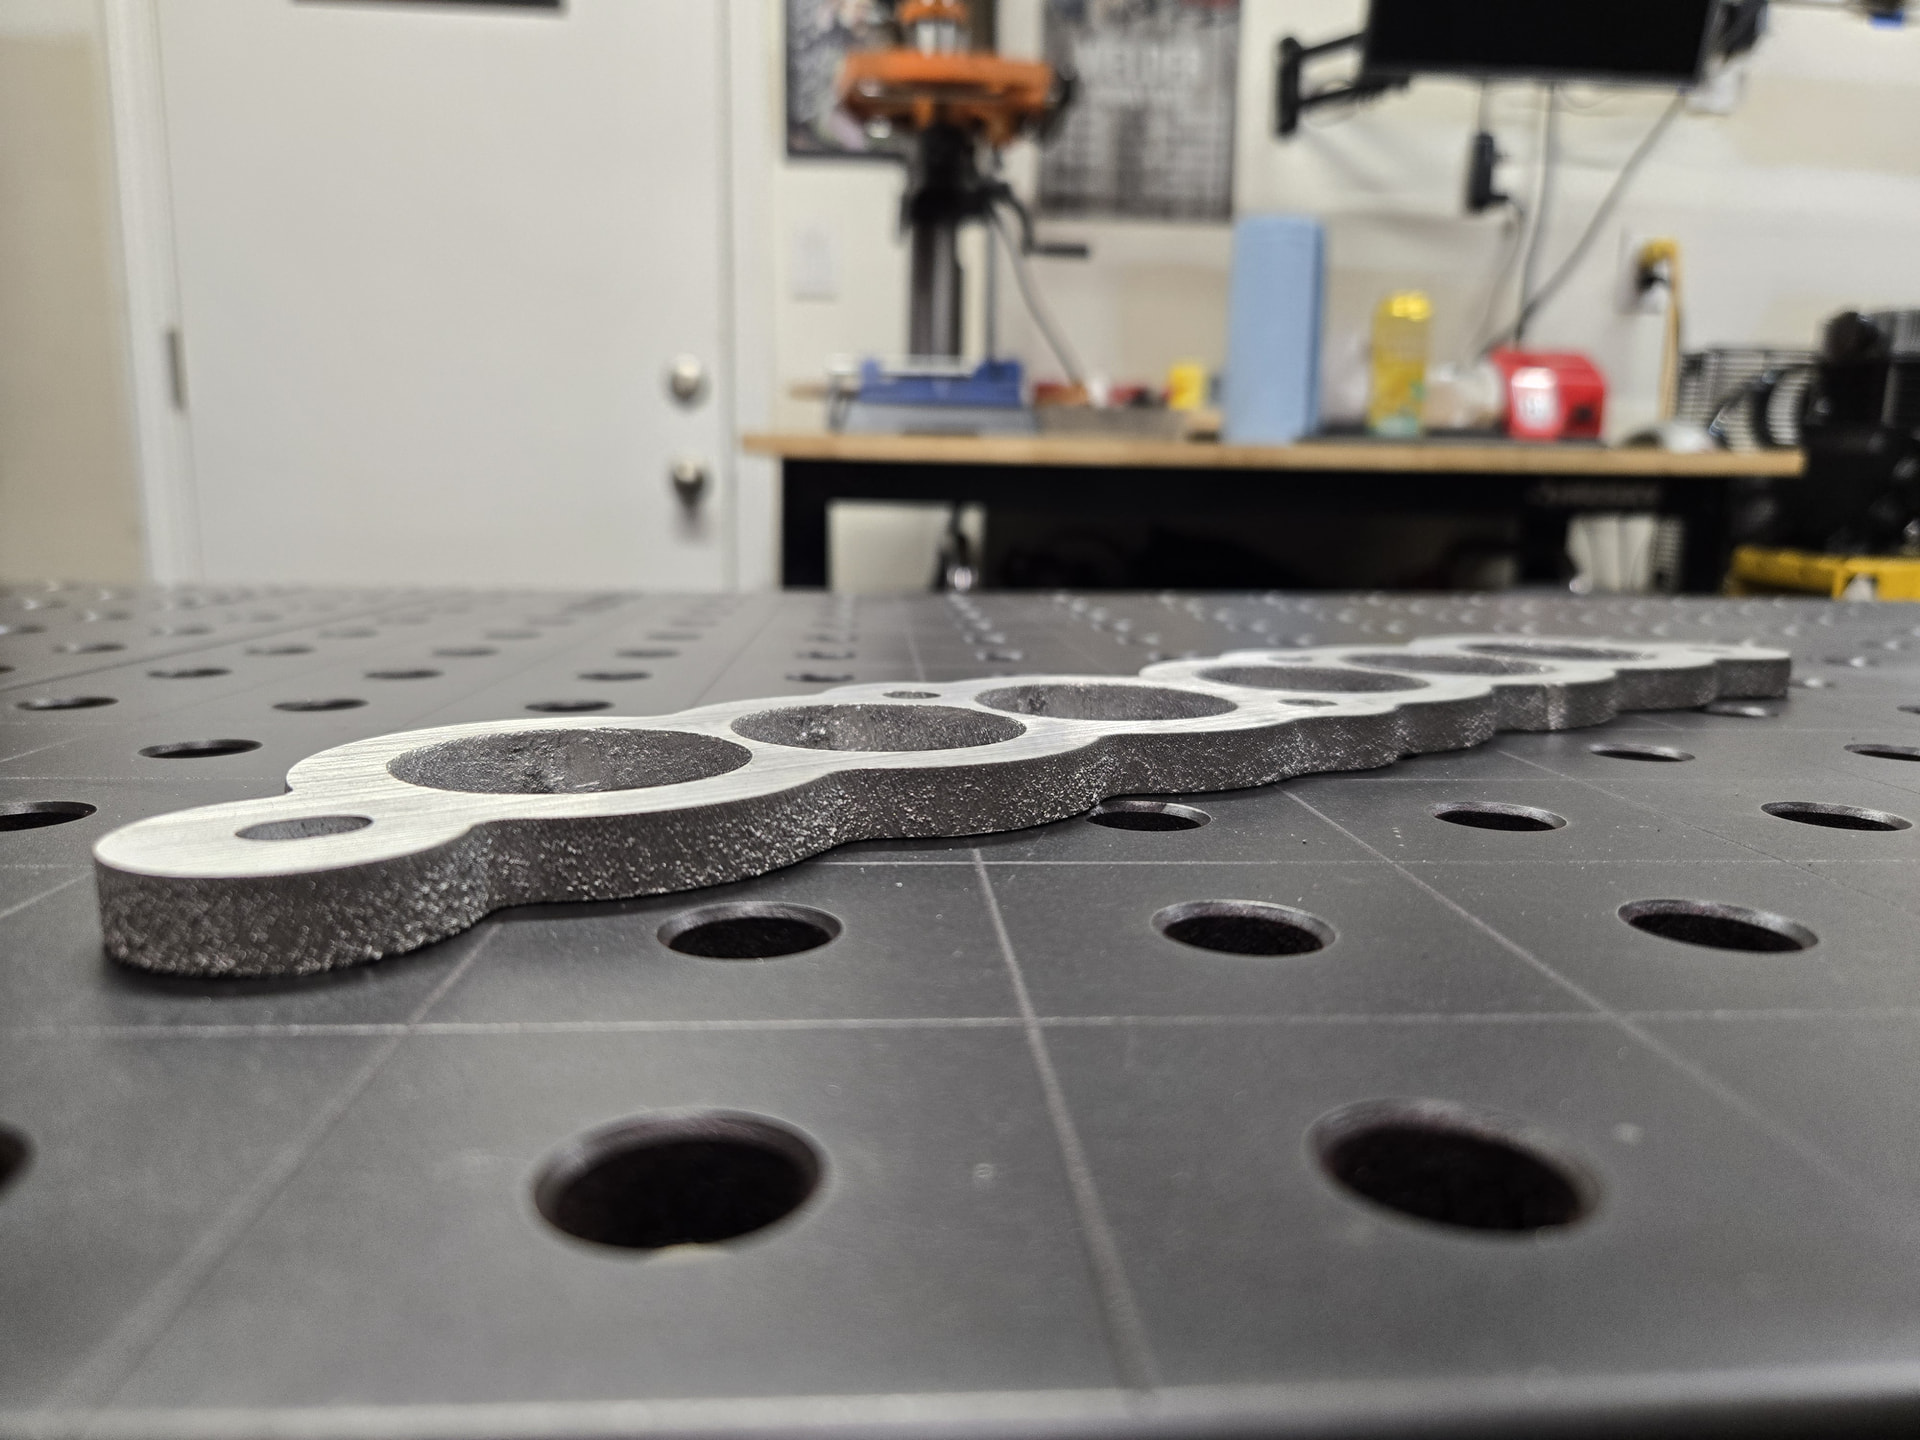
This is 1/4 @ 47 ipm with the same setting except 60 amps. Hypertherm cut chart say 38 to 40 ipm.

1 Like

Once you have verified that the work clamp is connected, if the issue persists, please email our support team. We will be happy to work with you to troubleshoot and help you get clean cuts.

1 Like

Looks like the electrode is bad. Does the arc look green? Like Big Daddy said, post some pics of the electrode and nozzle.

It should be cutting with those settings, so something is wrong with the plasma arc.

1 Like

Seems like a long pierce delay and slow cut speed.

I run 3/8" aluminum at 33ipm.

As others have stated, ensure your consumables aren’t bad and that your work clamp is connected directly onto the base of the material you’re cutting.

2 Likes

That table ever get used for anything other than pictures? :rofl: looks brand new!

2 Likes

You know I don’t get my hands dirty!

My shop is just for show :rofl:

Also verify your order of cut. You need to cut the pieces starting at the innermost one then proceed outward. If you try from outside in, you will have lost your electrical contact.