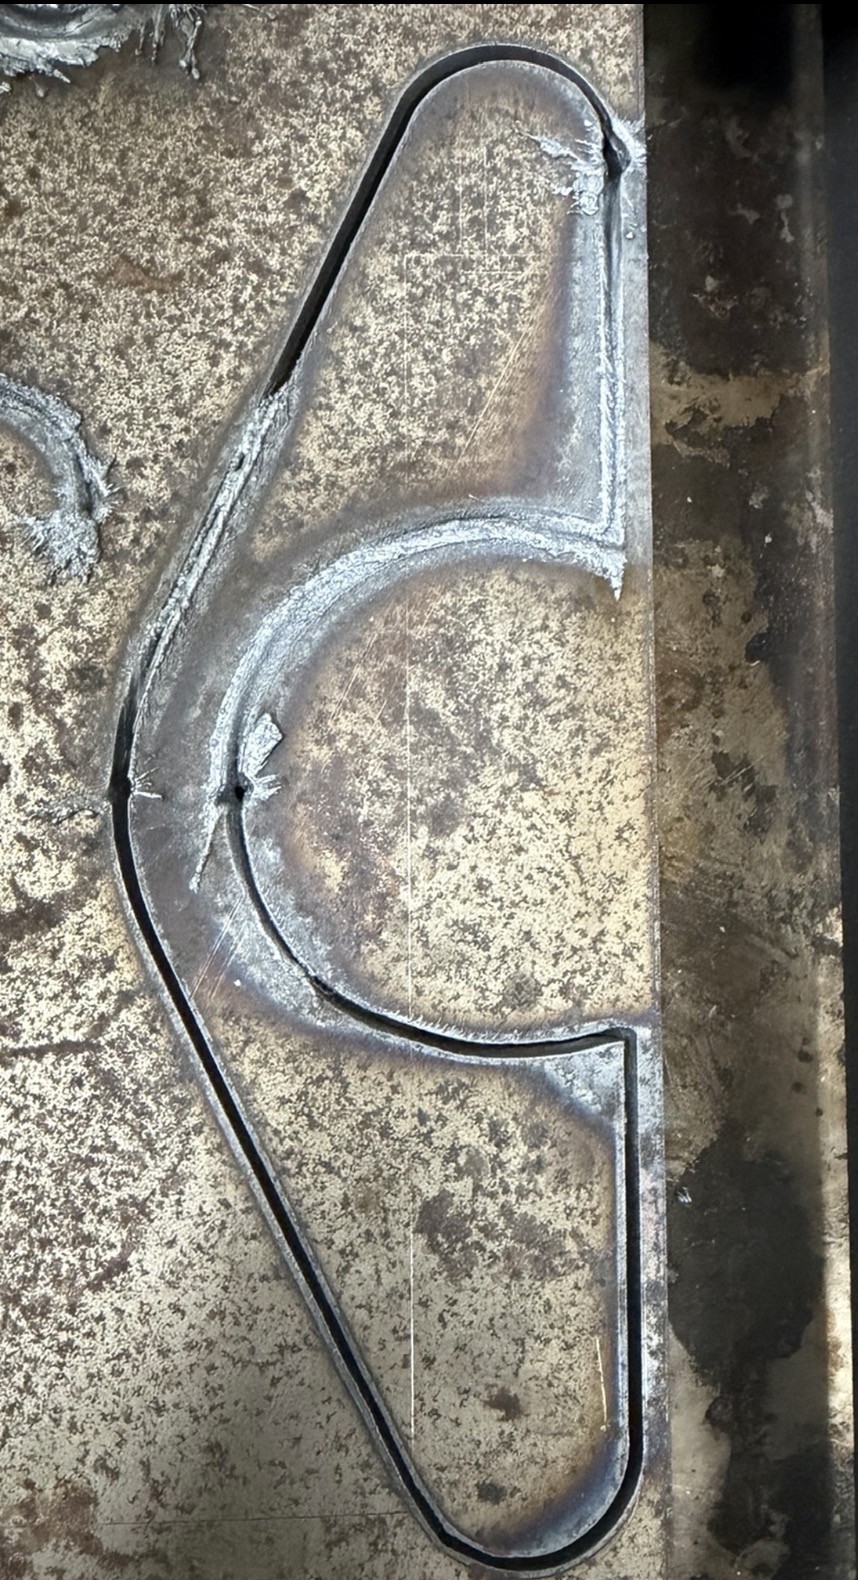
Anyone have any advice or help on this issue? My cuts start out fine and then do not cut all the way through the material. I’m running a hypertherm 45xp with z axis control. Cutting 1/4” steel with a feed rate of 48
1 Like
Why three pierce entries?
1. Send pictures of the ends of the torch consumables.
2. Is the work clamp on the metal you’re cutting?
3. Is your air pressure above 70 psi while it’s cutting?
We need more information, but we will start there.
Cut height, pierce height, 48 ipm sound reasonable.
3 Likes
Can you remember what you were cutting last, when the cut was acceptable?
I cut 1/4 inch mild steel at 40 ipm with 45 A on my razorweld. Low air pressure, worn nozzle can also contribute.
Potentially a bad ground connection. The cable itself or how it’s plugged in might be compromised.